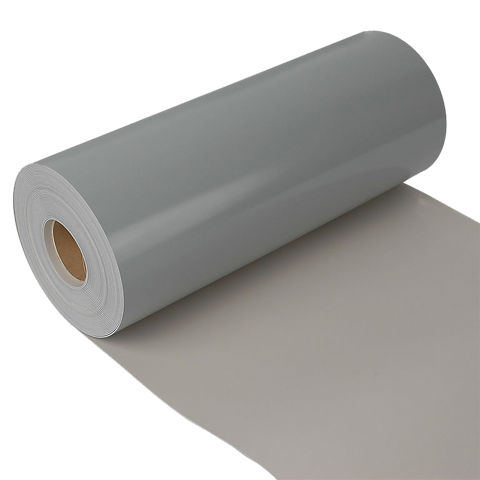
Sarnafil® T 66-15D, FPO Membrane for Details
SIKA
Sika is a global leader in specialty chemicals for the construction and industrial sectors. The company develops and supplies innovative products and systems for bonding, sealing, damping, reinforcing, and protecting structures. With a strong focus on sustainability and performance, Sika serves a wide range of applications including concrete production, waterproofing, roofing, flooring, and structural strengthening.
Read morePolymer membrane for details on roofs with Sarnafil® T membranes Sarnafil® T 66-15 D is an unreinforced multilayer synthetic membrane based on flexible polyolefin (FPO). Sarnafil® T 66-15 D is a membrane for detailing, heat-weldable with hot air and UV resistant. | |||||||||||||||||||||||||||||||||||||||||||||
UseMaking details for Sarnafil® T roofing membranes:
Advantages
packSarnafil® T 66-15 D membrane rolls are individually wrapped in blue PE foil.
Color
| |||||||||||||||||||||||||||||||||||||||||||||
Typical technical data
| |||||||||||||||||||||||||||||||||||||||||||||
ApplicationAmbient air temperature -20 °C (68 °F) min. / +60 °C (+140 °F) max. Support temperature -30 °C (86 °F) min. / +60 °C (+140 °F) max. EQUIPMENT Hot air thermowelding of overlaps Electric hot air welding equipment, such as manual hot air welding machines and pressure rollers or automatic hot air welding machines, with a controlled temperature of at least +600 °C (+1112 °F). Recommended equipment type: Manual: Leister Triac Automatic: Sarnamatic 661/681 Semi-automatic: Leister Triac Drive SUPPORT QUALITY The surface of the substrate must be even, smooth and free of sharp projections or burrs, etc. The substrate must be membrane compatible, solvent resistant, clean, dry and free from dust and grease. Metal surfaces must be degreased with Sarnafil® Cleaner before applying the adhesive. APPLICATION Application procedure Strictly follow the installation procedures defined in the application procedure, application manuals and work instructions which must always be adjusted to the actual site conditions. Reference should be made to the following application instructions: Sarnafil® T roofing systems. Fixing method The detailing membrane is heat-welded onto the already installed FPO roofing membrane. Thermowelding method Overlapping edges must be welded with electric hot air welding equipment. Welding parameters, including temperature, machine speed, air flow, pressure and welding machine settings must be evaluated, adapted and checked on site according to the type of equipment and climatic conditions, before starting heat welding. The effective width of heat-welded overlaps shall be a minimum of 20 mm (0.787 in). Welding testing Welds should be mechanically tested with a screwdriver (rounded edges) to ensure weld integrity / completion. Any imperfections must be repaired by hot air welding. |